Drive-in racking for heavy goods is considered the optimal storage solution for warehouses with high-volume pallet storage and a need to maximize space utilization. Thanks to its design that allows forklifts to drive deep inside to load and unload goods using the LIFO (Last-In, First-Out) principle, this system helps businesses reduce aisle space, increase storage density, and ensure superior load-bearing capacity.
This is a suitable choice for industries such as steel, wood, beverages, frozen food, or heavy industrial manufacturing, where stability, durability, and efficiency in warehouse management are required.
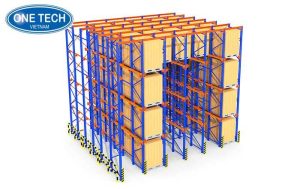
1. What is Drive-In racking for heavy goods?
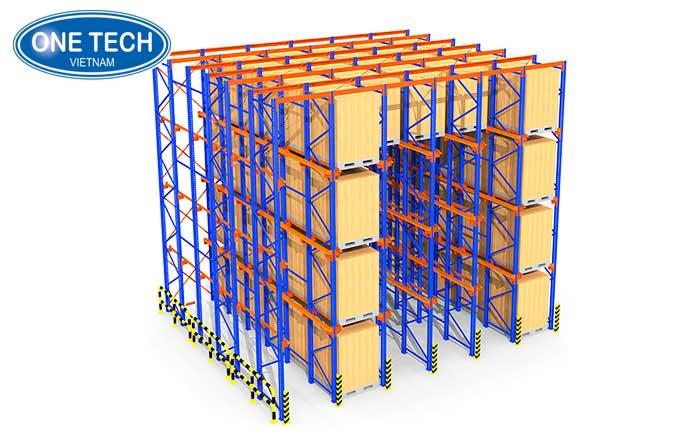
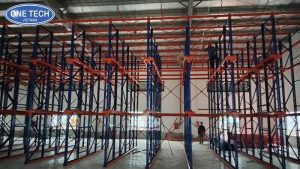
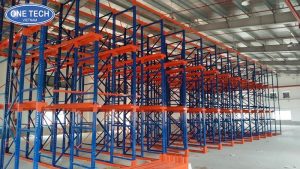
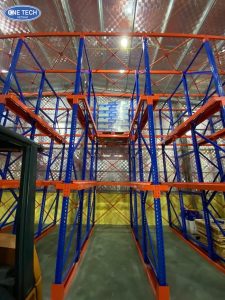
Drive-in racking for heavy goods is a warehouse racking system designed in a "basement" style with deep aisles, allowing forklifts to load pallets onto each level in a LIFO (Last-In, First-Out) manner. The entire structure is made of high-strength steel frame, optimized for storing heavy, high-load goods in warehouses with limited space.
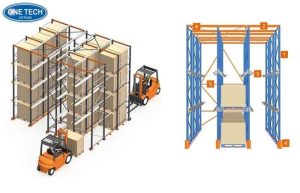
By eliminating aisles between rack rows, drive-in racking increases storage density many times compared to selective racking, suitable for businesses that need to group large quantities of the same SKU. This is a popular solution in cold storage, freezer, food storage, and industrial warehouses that require safe and centralized storage of high-load items.
2. Operating principle of Drive-In racking for heavy goods
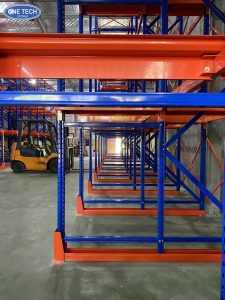
The operating principle of Drive-In racking for heavy goods is based on the LIFO (Last In – First Out) mechanism, where pallets are moved in the reverse order of entry; goods that entered later are moved out first. Specialized forklifts directly drive into each rack lane to place or retrieve pallets on the guide rail system, optimizing space and increasing storage density for heavy palletized goods.
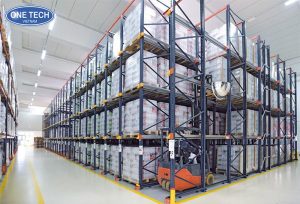
Compared to Selective racking, this system saves more space but has lower selectivity. Compared to Drive-Thru racking, industrial Drive-In racking only has one entry/exit point, making it suitable for homogeneous goods, while Drive-Thru supports two entry points for FIFO operation.
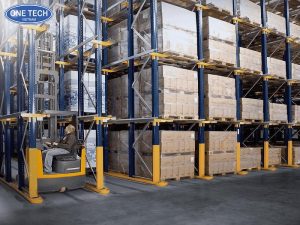
3. Features of Drive-In racking for heavy goods
Drive-in racking systems for heavy goods are designed with a deep-to-high structure, creating pallet lanes capable of handling heavy loads and operating stably in high-intensity storage environments.
The system focuses on optimizing space in depth, significantly reducing the number of aisles and increasing the number of pallets stored in the same area. This is a suitable option for businesses requiring a specialized storage solution for homogeneous, high-volume goods and batch-based sorting.
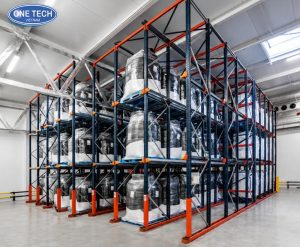
Key technical specifications of Drive-In racking for heavy goods:
- Design load: 800 – 2,000 kg/pallet depending on configuration.
- Shelf depth: 4 – 12 pallets/lane, adjustable according to warehouse space.
- System height: 3 – 10m, accommodating various types of forklifts.
- Column frame: High-strength steel, thickness 1.8 – 2.5mm.
- Pallet guide rails: Powder-coated steel.
- Standard paint colors: Blue-orange or as requested.
4. Outstanding advantages of Drive-In racking for heavy goods
When operating warehouses storing heavy palletized goods, Drive-In racking for heavy goods offers a significant advantage due to its durable and secure long-term storage capabilities. Its robust structure ensures stability even when the warehouse requires high and deep stacking, thereby creating a more concentrated and efficient storage space for businesses.
Key advantages:
- Increased storage density: Allows for deep storage of multiple pallets on the same lane, suitable for large quantities of heavy, packaged goods.
- Reduce aisle space – optimize area: Minimizing the space required for movement within the warehouse results in a more compact structure with increased storage capacity.
- Ideal for heavy and homogeneous goods: The system is designed for pallets of the same type, enabling fast and accurate inventory control.
- High durability, performs well in harsh environments: The heavy-duty steel frame, with its durable powder coating, withstands vibration, cold, humidity, or high operating frequency.
- Cost savings in operation: Optimizing space means reducing warehouse rental area, lowering handling costs, and improving overall operational efficiency.
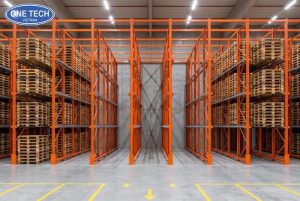
5. Purchase Drive-In racking for heavy goods at One Tech Rack
Purchasing Drive-In racking systems for heavy goods from One Tech Rack provides businesses with a professional, safe, and space-optimized storage solution right from the start. One Tech Rack offers racking systems designed to meet the specific load requirements of each warehouse, ensuring high durability and stability, and suitability even in harsh environments such as cold storage, freezer storage, or heavy industrial warehouses. Customers receive free consultation, site survey, 2D/3D design, and transparent pricing, ensuring efficient, stable, and safe operation of the Drive-In racking system throughout its lifespan.
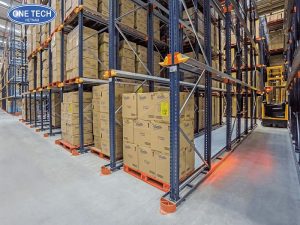
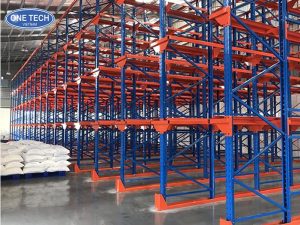
As the need for heavy pallet storage increases, choosing the right racking solution becomes crucial to ensuring safety, efficiency, and cost-effectiveness for businesses. Drive-in racking for heavy goods not only optimizes space but also creates a professional, stable, and long-lasting warehouse system. Investing wisely from the start will help businesses operate smoothly, protect goods, and improve warehouse management capabilities at every stage of development.